Pilling Resistance Solutions for Leggings: A Technical Guide
This guide sets out how pilling resistance can be engineered into high-waist leggings before bulk production begins.
How the problem appears in production
small fibre balls that make a garment look old is most obvious the knee and seat areas flex thousands of times a session. Buyers usually find it during fitting rather than in the lab, so early target setting matters. Because the knee and seat areas flex thousands of times a session, target checks are made on a worn sample rather than flat fabric alone.
Specification targets that work
Set the measurable target at grade 4 after 7000 revolutions. Without a number on the tech pack the mill chooses its own standard, which rarely matches the brand requirement. Keep ISO 12945-2 Martindale pilling box named in the tech pack so every lot is measured the same way.
Fabric and finish options
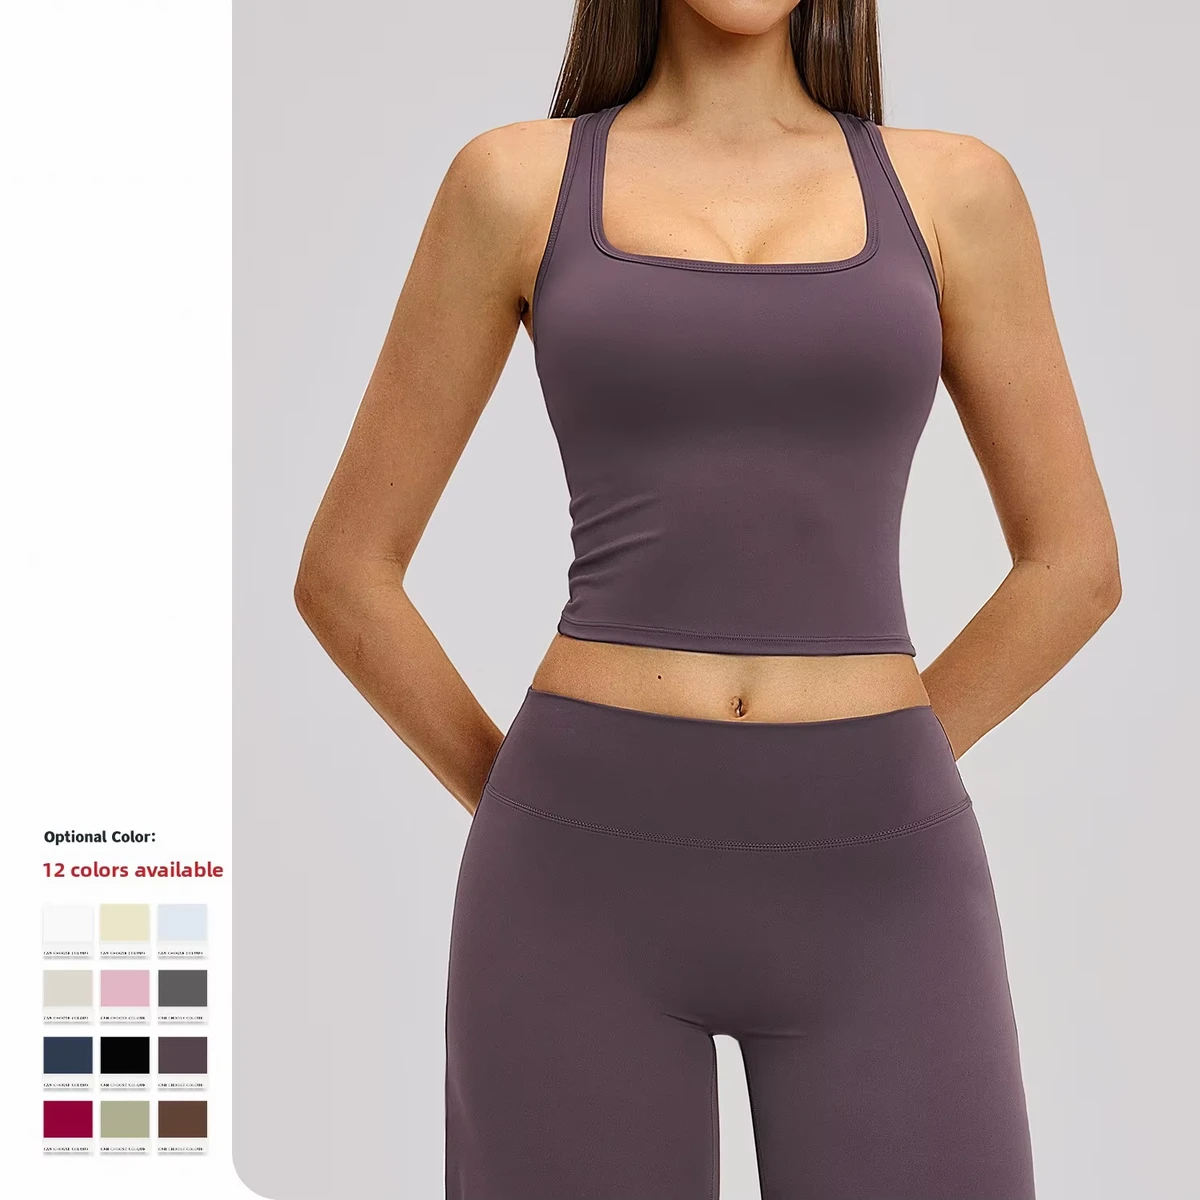
The practical route combines select higher twist count yarn, tighten stitch length and add singeing and apply an anti-pilling finish and heat set correctly. Options can be combined, but every added step needs extra approval time. Where high-waist leggings is worn for studio, running and strength sessions, set tolerances around that range of movement.
Construction details
Pattern and seam placement decide whether the fix survives wear. Because the high-waist leggings is used for studio, running and strength sessions, allow for worst-case load rather than average use. Any change to interlock or single jersey around 220-260 GSM requires re-testing against grade 4 after 7000 revolutions before bulk is released.
Validation before bulk
Approve against ISO 12945-2 Martindale pilling box and keep reports with the bulk file. A short pre-production run of 30-50 pieces exposes problems a lab sample cannot. Past reports from ISO 12945-2 Martindale pilling box help the mill reproduce the same recipe on the next order.




